
试生产控制程序中英文版本
3.5物料部负责所需材料的采购。
3.6 Quality Control Department/ Academy of Science take charge of inspecting and identifying the products in trial production.
3.1工程总监/技术总监负责批量试产的批准。
3.2 The Engineering Department/Central Research Institute takes charge of trial production application, organization and technical guidance, problem solving and tracking of the whole process. If the trial production is needed because Central Research Institute develops the projects, materials, the process documents or Control Lot Flow should be formulated and the Engineering Department takes charge of the evaluation and approval. If the trial production is for the process alteration by Engineering Department, the Control Lot Flow should be formulated.
采用批量生产时所用工装、设备、环境、人员、材料和工艺进行试生产,从而达到验证,确认设计、设计过程更改有效性。
2、Scope/适用范围
It is applicable to trial production for new product design and development, and when necessary in modification of design/ process of the company’s lithium-ion battery.
In principle, the quantity of small battery for trial production is 1000-5000pcs (not include 1000pcs), big battery is 200-1000pcs (not include 200pcs). Customer’s delivery demand is taken into consideration if necessary. It is applied by Market Department, and not restrained.
File Name
文件名称
Trial Production Control Procedure
试生产控制程序
File NO.
文件编号
MP/Q 17-L
Edition版次
A/2
Page页次
1/10
Modification History Records修改历史纪录
Edition版次
Modification Description
适用于本公司聚合物锂电设计开发新产品的试产、设计/过程更改中有需要的试产。
3、Responsibility/职责
3.1 Chief Engineering Officer/Chief Technique Officer takes charge of approving mass trial production.
Adopt the tooling, equipment, environment, personnel, material and process used in mass production to trial produce, so as to verify the design and confirm the effectiveness of design process.
修改描述
Issue Date
发行日期
Author/Signature
作者/签名
File Name
文件名称
Trial Production Control Procedure
试生产控制程序
File NO.
文件编号
MP/Q 17-L
Edition版次
A/2
Page页次
2/10
1、The purpose/的
3.3工程部须保证整个量产过程中设备的正常运转;
3.4 Manufacturing Department takes charge of the organization and implementation of mass trial production.
3.4生产部负责批量试生产的组织和实施。
3.2工程部/中央研究院负责试产的申请、试产的组织及试生产的技术指导、问题的解决和整个过程的跟进。中央研究院因项目、材料开发需要试产时,制定工艺文件或《Control lot flow》由工程部负责审核、批准。工程部因过程更改试产时,制定《Control lot flow》;
3.3 The Engineering Department should guarantee the normal operation of equipments in the whole mass production process.
3.6品质部/中央研究院负责试产产品的检测和鉴定。
File Name
文件名称
Trial Production Control Procedure
试生产控制程序
File NO.
文件编号
MP/Q 17-L
Edition版次
A/2
Page页次
3/10
4、Definition (none)/定义(无)
Trial production quantity/试产数量:
控制计划(中英文标准模板)

容量Size 频率Freq.入库move to storage材料规格、数量Material Specificationquantity送货单Bills of dilivery1每批per lot到货计划Material planA-1◇C≤0.15、Si≤0.05、Mn≤0.60、S≤0.035、P≤0.035化学成分分析Chemical elementanalysis1每批per lotA-2◇抗拉强度Tensile strength ≥305Mpa、屈服强度Yield strength≥175Mpa、断后伸长率Elongation≥29力学性能分析Mechanical propertiesanalysis1每批per lot2.5±0.20-25mm(0.001)外径千分尺outside micrometer3每批per lot1250(+10,0)2600(+40,0)0-3m(1)卷尺Tape measure3每批per lot存放Storage275±10-300mm(0.02)游标卡尺Calipers无毛刺No Burr目视Visual设备间隙Shears gap0.2(+0.05,0)目测设备间隙参数设定Visual equipment gapparameter settings1每班Every shift调整设备、上报Adjustment equipment ,reporting φ265±0.50-300mm(0.02)游标卡尺Calipers无毛刺No Burr目视Visualφ141.5(+1.0,0)0-150mm(0.02)游标卡尺Calipers50.5(+1.5,-1.0)0-300mm(0.02)高度尺Height Gages高度Height 首末检1件、巡检3件、自检3件first and endinspection1pcs,inspection3pcs,self-inspection 3pcs首末检1次、巡检每4小时、自检每1小时first and endinspection1,inspection every4hrs,self-inspectionevery hrs检验记录Inspectionrecord标识、隔离、检查模具Identification ,Separate ,Checkthe die供方/工厂Supplier/Plant:山东慧达汽车部件有限公司Shandong HuiDa Automotive Parts Co., Ltd.其它批准/日期(如需要)Other Approval/Date(If Req'd)标识、隔离、调整设备Identification ,Separate,Adjustment device 生产设备Machine.DeviceJig.ToolsFor Mfg.特性Characteristics零件名称/描述Part Name/Description 端盖HP HUB CAP,GREASE NON-VENTEDJY32-315/315T油压机Hydraulic Press直径Diameter40冲压拉深成形Punch供方/工厂批准/日期Supplier/Plant Approval/Date过程名称/操作描述Process Name/OperationDescriptionHD130-H002/拉深模Drawing Die条料宽度尺寸Material widthdimension其它批准/日期(如需要)Other Approval/Date (If Req'd)检验记录Inspectionrecord用户工程批准/日期(如需要)User Engineering Approval/Date (If Req'd)用户质量批准/日期(如需要)User Quality Approval/Date (If Req'd)聂建钦,彭亮,李庆平,刘客,张守东,张栋,苗秀宝、王树龙供方代号Supplier Code零件号/最新更改水平Part Number/Latest Change LevelE32629-1、E32629-3零件/过程编号Part/ Process Number评价/测量技术EvaluationMeasurementTechnique样本Sample控制方法ControlMethod特殊特性分类SpecialChar.Class方法Methods标识、隔离、退货Identification ,Separate ,Reject产品标识和防护控制程序 HD/PF02-SP09Product identification and protection control program反应计划Reaction Plan 编号NO.产品Product过程Process产品/过程/规范/公差Product/ProcessSpecification/Tolerance10原材料入厂检验Receiving Raw material and Inspection力学性能Mechanicalproperties原材料检验报告Raw materialsinspectionreport原材料长/宽尺寸Length/widthdimensions原材料检验记录Raw materialinspectionrecords化学成分chemical element原材料厚度尺寸thicknessdimension20剪板机下料Shears CuttingQC12Y-12*2500/液压剪板机Hydraulic shears外观Appearance首末检1件、巡检3件、自检3件first and endinspection1pcs,inspection3pcs,self-inspection 3pcs首末检1次、巡检每4小时、自检每1小时first and endinspection1,inspection every4hrs,self-inspectionevery hrs30冲压落料Punch首末检1件、巡检3件、自检3件first and endinspection1pcs,inspection3pcs,self-inspection 3pcs首末检1次、巡检每4小时、自检每1小时first and endinspection1,inspection every4hrs,self-inspectionevery hrs检验记录Inspectionrecord标识、隔离、检查模具Identification ,Separate ,Checkthe die外观AppearanceJA21-160/160T冲床PressesHD110-H009/落料模Blanking die直径Diameter容量Size频率Freq.供方/工厂Supplier/Plant:山东慧达汽车部件有限公司Shandong HuiDa Automotive Parts Co., Ltd.其它批准/日期(如需要)Other Approval/Date(If Req'd)生产设备Machine.Device Jig.Tools For Mfg.特性Characteristics 零件名称/描述Part Name/Description端盖HP HUB CAP,GREASE NON-VENTED供方/工厂批准/日期Supplier/Plant Approval/Date 过程名称/操作描述Process Name/OperationDescription其它批准/日期(如需要)Other Approval/Date (If Req'd)用户工程批准/日期(如需要)User Engineering Approval/Date (If Req'd)用户质量批准/日期(如需要)User Quality Approval/Date (If Req'd)聂建钦,彭亮,李庆平,刘客,张守东,张栋,苗秀宝、王树龙供方代号Supplier Code零件号/最新更改水平Part Number/Latest Change Level E32629-1、E32629-3零件/过程编号Part/Process Number评价/测量技术Evaluation Measurement Technique样本Sample控制方法Control Method特殊特性分类SpecialChar.Class方法Methods反应计划Reaction Plan编号NO.产品Product过程Process产品/过程/规范/公差Product/ProcessSpecification/Tolerance47±10-300mm(0.02)深度尺Depth Gages首末检1件、巡检5件、自检5件first and end inspection 1pcs,inspection 5pcs,self-inspection 5pcs首末检1次、巡检每2小时、自检每1小时first and end inspection 1,inspection every 2hrs,self-inspectionevery hrs标识、隔离、检查模具Identification ,Separate ,Checkthe die B-1压力Pressure◇上缸Cylinder 15(+1,0)Mpa下缸Undercylinder9(+1,0)Mpa目视Visual1每班Every shift调整设备、上报Adjustment equipment ,reportingφ142.5(+0.2,-0.3)0-150mm(0.02)游标卡尺Calipers 50.5(+1.5,-2.0)0-300mm(0.02)高度尺Height GagesA-3◇47±10-300mm(0.02)深度尺Depth Gages首末检1件、巡检5件、自检5件first and end inspection 1pcs,inspection 5pcs,self-inspection 5pcs首末检1次、巡检每2小时、自检每1小时first and end inspection 1,inspection every 2hrs,self-inspectionevery hrs标识、隔离、检查模具Identification ,Separate ,Checkthe die B-1压力Pressure◇上缸Cylinder 15(+1,0)Mpa下缸Undercylinder9(+1,0)Mpa目视Visual1每班Every shift调整设备、上报Adjustment equipment ,reportingφ214±0.50-300mm(0.02)游标卡尺Calipers6×φ8.7±0.250-150mm(0.02)游标卡尺Calipers A-4◇HDJ-H0001检具Gage首末检1件、巡检5件、自检5件first and end inspection 1pcs,inspection 5pcs,self-inspection 5pcs末检1次、巡检每2小时、自检每1小时first and end inspection 1,inspection every 2hrs,self-inspectionevery hrsφ205±0.750-300mm(0.02)游标卡尺Calipers 深度Depth检验记录Inspection record50整形ShapingJY32-315/315T油压机Hydraulic Press 直径Diameter 首末检1件、巡检3件、自检3件first and end inspection 1pcs,inspection 3pcs,self-inspection 3pcs 首末检1次、巡检每4小时、自检每1小时first and end inspection 1,inspection every 4hrs,self-inspectionevery hrs 检验记录Inspection recordHD134-H014/整形模Shaping Die高度Height检验记录Inspection record标识、隔离、检查模具Identification ,Separate ,Checkthe die孔径diameter I.D.HD146-H011/切边冲孔模Trimming and Punching die位置度Location degreeJA21-160/160T冲床Presses深度Depth直径Diameter 检验记录Inspection record标识、隔离、检查模具Identification ,Separate ,Checkthe die40冲压拉深成形Punch冲压切边冲孔Trimming and PunchingJB21-160B-SM/160T冲床直径Diameter首末检1件、巡检3件、自检3件first and endinspection首末检1次、巡检每4小时、自检每1小时first and end inspection60首末检1件、巡检3件、自检3件first and end inspection 1pcs,inspection3pcs,self-inspection 3pcs首末检1次、巡检每4小时、自检每1小时first and end inspection 1,inspection every 4hrs,self-inspectionevery hrs容量Size频率Freq.供方/工厂Supplier/Plant:山东慧达汽车部件有限公司Shandong HuiDa Automotive Parts Co., Ltd.其它批准/日期(如需要)Other Approval/Date(If Req'd)生产设备Machine.Device Jig.Tools For Mfg.特性Characteristics 零件名称/描述Part Name/Description端盖HP HUB CAP,GREASE NON-VENTED供方/工厂批准/日期Supplier/Plant Approval/Date 过程名称/操作描述Process Name/OperationDescription其它批准/日期(如需要)Other Approval/Date (If Req'd)用户工程批准/日期(如需要)User Engineering Approval/Date (If Req'd)用户质量批准/日期(如需要)User Quality Approval/Date (If Req'd)聂建钦,彭亮,李庆平,刘客,张守东,张栋,苗秀宝、王树龙供方代号Supplier Code零件号/最新更改水平Part Number/Latest Change Level E32629-1、E32629-3零件/过程编号Part/Process Number评价/测量技术Evaluation Measurement Technique样本Sample控制方法Control Method特殊特性分类SpecialChar.Class方法Methods反应计划Reaction Plan编号NO.产品Product过程Process产品/过程/规范/公差Product/ProcessSpecification/Tolerance10(+2,0)0-300mm(0.02)高度尺Height Gages85°±0.5°0-360°(2′)万能角度尺Universal angle rulerA-5◇首末检、巡检0-10mm(0.01)百分表/自检 0-1mm塞尺First and endinspection 0-10mm(0.01) Dialindicator/Self-inspection 0-1mmFeeler首末检1件、巡检5件(X-R图)、自检5件first and end inspection 1pcs,inspectio n 5pcs(X-R chart),self-inspection 5pcs末检1次、巡检每2小时、自检每1小时first and endinspection1,inspection every2hrs,self-inspection everyhrsφ4(+2,-1)0-150mm(0.02)游标卡尺Calipers 1±0.250-300mm(0.02)高度尺Height Gages90无油污No dirt 目测Visual全检Full inspection每批per lot检验记录Inspection record 标识、隔离、退货Identification ,Separate ,Reject喷塑气压Spray pressure0.4-0.5MPa喷塑电压Spray voltage 50-60KV烘烤温度Bakingtemperature 180-200℃烘烤时间Baking time30-40min 无漏喷No leakage jet目测Visual调整设备、上报Adjustment equipment ,reporting100喷塑SprayXNG-36-1B/粉末喷涂生产线Powder coating production lines目测Visual1产线外观Appearance全检Full inspectionper lot70冲压翻边成形FlangingJB21-160B-SM/160T冲床Presses件、自检3件first and end inspection 1pcs,inspection 3pcs,self-inspection 3pcs时、自检每1小时first and end inspection 1,inspection every 4hrs,self-inspectionevery hrs80冲压压字Pressure logoJA21-160/160T冲床Presses孔径diameter I.D.首末检1件、巡检3件、自检3件first and end inspection 1pcs,inspection 3pcs,self-inspection 3pcs标识、隔离、检查模具Identification ,Separate ,Checkthe die角度AngleHD124-H008/翻边模Flanging die平面度Flatness高度Height 标识、隔离、检查模具Identification ,Separate ,Checkthe dieHD150-H006/压字模Pressure logo die(E32629-3)HD150-H005/压字模Pressure logo die(E32629-1)高度Height检验记录Inspection record首末检1次、巡检每4小时、自检每1小时first and end inspection 1,inspection every 4hrs,self-inspectionevery hrs检验记录Inspection record外观Appearance外协镀锌Outsourcing galvanized检验记录Inspection record每班Every shift检验记录Inspection record容量Size频率Freq.供方/工厂Supplier/Plant:山东慧达汽车部件有限公司Shandong HuiDa Automotive Parts Co., Ltd.其它批准/日期(如需要)Other Approval/Date(If Req'd)生产设备Machine.Device Jig.Tools For Mfg.特性Characteristics 零件名称/描述Part Name/Description端盖HP HUB CAP,GREASE NON-VENTED供方/工厂批准/日期Supplier/Plant Approval/Date 过程名称/操作描述Process Name/OperationDescription其它批准/日期(如需要)Other Approval/Date (If Req'd)用户工程批准/日期(如需要)User Engineering Approval/Date (If Req'd)用户质量批准/日期(如需要)User Quality Approval/Date (If Req'd)聂建钦,彭亮,李庆平,刘客,张守东,张栋,苗秀宝、王树龙供方代号Supplier Code零件号/最新更改水平Part Number/Latest Change Level E32629-1、E32629-3零件/过程编号Part/Process Number评价/测量技术Evaluation Measurement Technique样本Sample控制方法Control Method特殊特性分类SpecialChar.Class方法Methods反应计划Reaction Plan编号NO.产品Product过程Process产品/过程/规范/公差Product/ProcessSpecification/ToleranceA-5◇0.15mm塞尺(端盖平放在大理石台面,上面压5kg物体)/0.15mm feeler ( cover flat on the marble countertops, pressure5kg objects above )盐雾试验≥1000小时/Salt spray test≥1000hrs盐雾腐蚀试验机/Salt spray corrosiontest machine3每季度Each quarter 盐雾试验报告Salt spray testreport 110丝印完整Full screen目测Visual全检Full inspection每批per lot检验记录Inspection record标识、隔离、退货Identification ,Separate ,RejectA-3◇47±10-300mm(0.02)深度尺Depth Gages10A-4◇HDJ-H0001检具Gage 10A-5◇0.15mm塞尺(端盖平放在大理石台面,上面压5kg 物体)/0.15mm feeler (cover flat on the marble countertops,pressure 5kg objectsabove )10包装规范Packaging Specifications点数Counting 2箱2 box标识、隔离、返工Identification ,Separate ,Rework清晰Clear 目测Visual 包装规范Packaging Specifications 目测Visual 物资发货单Material Invoice点数Counting标识、隔离、返工Identification ,Separate ,Rework平面度Flatness防腐蚀性能Corrosion100喷塑SprayXNG-36-1B/粉末喷涂生产线Powder coating production lines全检Full inspection每批per lot外协丝印Outsourcing Screen外观Appearance 检验记录Inspection record深度Depth120抽检并包装Sampling inspection and packaging标识、隔离、处理Identification ,Separate ,Dealwith位置度Location degree平面度Flatness数量Quantity 每批per lot检验记录Inspection record标识Label标识、隔离、返工Identification ,Separate ,Rework包装Package 数量Quantity130入库&出货Warehousing & shipping全检Full inspection每批per lot 物资发货单Material Invoice。
控制计划控制程序(中英文)
控制计划控制程序(IATF16949-2016)1、目的1. Purpose对控制零件和过程的体系,通过控制特性的过程监视和控制方法来最大限度地减少过程和产品变差;并随着测量系统和控制方法的评价和改进对其进行修订,使控制计划在整个产品寿命周期中得到保持和使用,确保按顾客的要求制造出优质的产品。
It aims to control the part and process systems and reduce process and product variations to the utmost extent through process monitoring and control methods of the control characteristics; the control plan shall be revised along with the evaluation and improvement of the measurement system and the control methods and shall be maintained and used in the whole product life cycle so as to ensure that high qualify product is manufactured according to the requirements of the customer.2、适用范围2. Scope适用于本公司内产品的样件、小批量试产和批量生产所用的控制计划。
如客户有特殊要求,必须按照客户的要求执行。
It applies to the control plans used in the product sample, small-lot trial production and volume production of the company. If the customerhas special requirements, it shall be implemented according to the requirements of the customer.3、定义3. Definition无None4、职责4. ResponsibilitiesAPQP项目小组负责控制计划的策划,质量部负责编制与维护The APQP project team shall be responsible for planning of the control plan and the quality department shall be responsible for preparation and maintenance of it.5、程序5. Procedure5.1 当顾客和公司有需求和要求时,项目小组在不同阶段制订出相应的控制计划(即:样件控制计划、试生产控制计划、生产控制计划),项目组按工艺文件将其发行至相关部门,由其执行。
试生产控制计划范例(英文版)
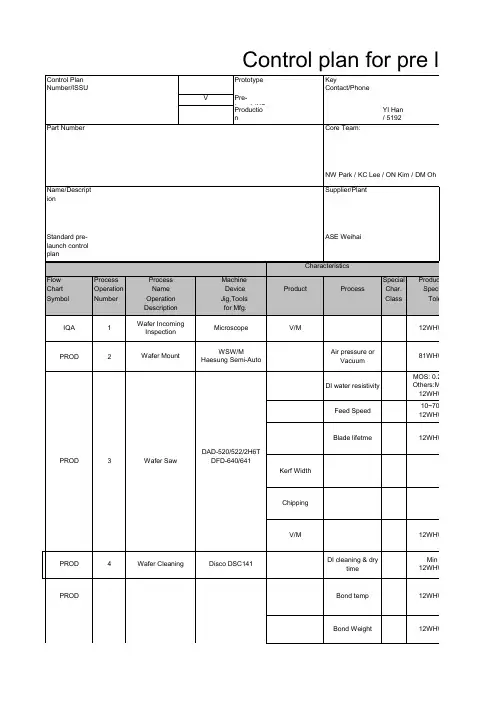
Log Sheet
Adjust
12WHW30002A
Dage Tester
10 balls
WHQ-6010
Die temp
81WHW40001A
ቤተ መጻሕፍቲ ባይዱ
Transfer pressure Transfer time PROD 7 Mold Fuse, Kotaki Clamp pressure Cure time Preheater condition V/M Delamination(Pro cess/QA eng'r confirm) PROD 8 PMC Wansan Deflash Machine Temp & Duration C-D/FTemp. C-D/F Time E-D/F Voltage
V/M
12WHW92106A
Al wire: M7200 plus, M360 Loop height PROD 6 Wire Bond Au wire : SWB700D/S, SWB-FA-UTC-10 Cu wire Eagle 60/AP
Wire pull test(Process/QA eng'r confirm)
Date(Orig.) Date(Rev.) Customer Engineering Approval(if Req'd) Kim / DM Oh Supplier Code Customer Quality Approval/Dtae(if Req'd) Sample Product/Process Specification/ Tolerance Evaluation Measurement Technique Control Method Reaction Plan
中英文对照版-生产计划控制程序
ABC用品有限公司质量管理体系程序文件编制: 日期:审核: 日期:批准: 日期:发放范围:公司各部门2013年10月01日生效1 目的Objective对生产计划及进度进行控制,确保生产按计划顺利执行,确保能够按照顾客的要求及时发运、交付产品。
The objective of this procedure is to control the production plan and progress, to ensure the successful implementation of production plan, and to ensure the timely shipment and deliv ery of products per the customer's requirements.2 适用范围Applicable Scope适用于本公司所有产品的生产安排。
This is applicable to the production planning of all AICQ products.3 职责Responsibilities3.1 生产计划员负责编制公司生产计划,部门经理负责审核。
The production planner is responsible to formulate the company production plan. The department manager is responsible for audit.3.2 生产计划员按项目计划编制新产品试生产计划,批生产计划。
The production planner is responsible to formulate the trial production and batch production plan for the new product per the project plan.3.3 生产计划员按制造部工艺验证、工装验证计划编制新产品、新工艺的工艺和工装验证生产计划。
(完整版)控制计划中英文版
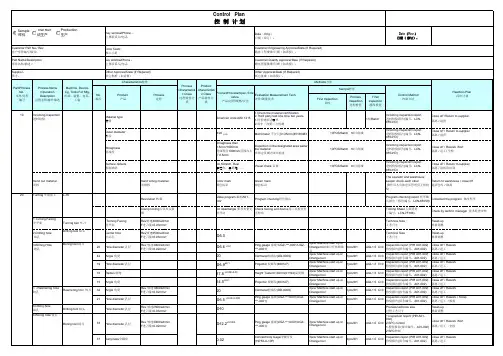
Sample 样件Trial Run试生产Production生产7.Turning OutsideDiameter车外圆Turning tool 车刀4Outside diameter 外径Rev 转速2500rad/min Φ14.03Projector 投影仪(490127)3pcs/ Machine start up orChange tool1pcs/3H AQL1.5 C=0Inspection report (PIR A01-002)检验报告(报告编号:A01-002)Inspection report (PIR A01-Close off / Rework隔离 / 返工Chamfer 倒角F进刀量=0.03mm/r 1.4±0.015Projector 投影仪(490127)3pcs/ Machine start up orChange tool 3只/开机和换刀3pcs/3H AQL1.0 C=01.Inspection report (PIR A01-002)2.SPC control1.检验报告(报告编号:A01-002)2.SPC控制Close off / Rework隔离 / 返工5Outside diameter 外径Φ12.6±0.03Projector 投影仪(490127)3pcs/ Machine start up orChange tool 1pcs/3H AQL1.5 C=0Inspection report (PIR A01-002)检验报告(报告编号:A01-002)Close off / Rework隔离 / 返工1Outside diameter 外径Φ16.18 0/-0.04Micrometer 千分尺(0~25mm)451384833pcs/ Machine start up orChange tool 3只/开机和换刀3pcs/3H AQL1.0 C=01.Inspection report (PIR A01-002)2.SPC control1.检验报告(报告编号:A01-002)2.SPC控制Close off / Rework隔离 / 返工25Angle 角度45.6°±5°Projector 投影仪(490127)3pcs/ Machine start up orChange tool 1pcs/3H AQL1.5 C=0Inspection report (PIR A01-002)检验报告(报告编号:A01-002)Close off / Rework隔离 / 返工8.Cutting Groove 割槽Cutting tool 切断刀2Outside diameter 外径Rev 转速2500rad/minФ 14+0.05Micrometer 千分尺(0~25mm)451384833pcs/ Machine start up orChange tool1pcs/3H AQL1.5 C=0Inspection report (PIR A01-002)检验报告(报告编号:A01-002)Close off / Rework /Sort隔离 / 返工/全检38Roughness 粗糙度F进刀量=0.03mm/r Ra1.6Roughness Tester 粗糙度仪DTS03A3pcs/ Machine start up orChange tool1pcs/3H AQL1.5 C=0Inspection report (PIR A01-002)检验报告(报告编号:A01-002)Close off / Rework隔离 / 返工11Width宽度 2.2 +0.2/0Height Tester0~30mm(01194)高度规3pcs/ Machine start up orChange tool1pcs/3H AQL1.5 C=0Inspection report (PIR A01-002)检验报告(报告编号:A01-002)Close off / Rework隔离 / 返工8Length 长度11.8±0.2Projector 投影仪(490127)3pcs/ Machine start up orChange tool1pcs/3H AQL1.5 C=0Inspection report (PIR A01-002)检验报告(报告编号:A01-002)Close off / Rework隔离 / 返工41Angle 角度3°±1°Projector 投影仪(490127)3pcs/ Machine start up orChange tool1pcs/3H AQL1.5 C=0Inspection report (PIR A01-002)检验报告(报告编号:A01-002)Close off / Rework隔离 / 返工26Radius圆弧R0.1 +0.1(2X)Projector 投影仪(490127)3pcs/ Machine start up orChange tool1pcs/3H AQL1.5 C=0Inspection report (PIR A01-002)检验报告(报告编号:A01-002)Close off / Rework隔离 / 返工9.Cutting off 切断Cutting tool 切断刀17Length 长度Rev 转速2500rad/minF进刀量=0.03mm/r23.4±0.1Height Tester0~30mm(01194)高度规3pcs/ Machine start up orChange tool1pcs/3H AQL1.5 C=0Inspection report (PIR A01-002)检验报告(报告编号:A01-002)Close off / Rework隔离 / 返工10.Drilling hole 钻孔Drilling tool 钻头22Inside diameter 外径Rev 转速2500rad/minΦ6+0.1Ping gauge 塞规(UGZ-***-0001/UGZ-***-0001)3pcs/ Machine start up orChange tool1pcs/3H AQL1.5 C=0Inspection report (PIR A01-002)检验报告(报告编号:A01-002)Close off / Rework隔离 / 返工36Concentricity 同轴度Φ0.02Concentricity Gage同轴度仪(19753-A-10P)3pcs/ Machine start up orChange tool3pcs/3H AQL1.0 C=0Inspection report (PIR A01-002)检验报告(报告编号:A01-002)Close off / Rework隔离 / 返工40Roughness 粗糙度F进刀量=0.03mm/r Ra6.3Roughness Tester 粗糙度仪DTS03A3pcs/ Machine start up orChange tool1pcs/3H AQL1.5 C=0Inspection report (PIR A01-002)检验报告(报告编号:A01-002)Close off / Rework隔离 / 返工14Length 长度9±0.25Projector 投影仪(490127)3pcs/ Machine start up orChange tool1pcs/3H AQL1.5 C=0Inspection report (PIR A01-002)检验报告(报告编号:A01-002)Close off / Rework隔离 / 返工33Angle 角度118°±3°Contracer轮廓仪(DD-0009)3pcs/ Machine start up orChange tool1pcs/3H AQL1.5 C=0Inspection report (PIR A01-002)检验报告(报告编号:A01-002)Close off / Rework隔离 / 返工31Chamfer 倒角0.2 +0.2/0.1*45Projector 投影仪(490127)3pcs/ Machine start up orChange tool1pcs/3H AQL1.5 C=0Inspection report (PIR A01-002)检验报告(报告编号:A01-002)Close off / Rework隔离 / 返工11.Drilling hole 钻孔Drilling tool 钻头Hole diameter 孔径Rev 转速2500rad/minF进刀量=0.03mm/rΦ10Process technice size过程工艺尺寸Reset-up重新调整12.Boring Hole镗孔Boring tool 镗刀23Inside diameter 外径Rev 转速3000rad/minF进刀量=0.02mm/rΦ8.8±0.1Ping gauge 塞规(UGZ-***-0001/UGZ-***-0001)3pcs/ Machine start up orChange tool1pcs/3H AQL1.5 C=0Inspection report (PIR A01-002)检验报告(报告编号:A01-002)Close off / Rework隔离 / 返工30Chamfer 倒角0.1*45°Projector 投影仪(490127)3pcs/ Machine start up orChange tool 1pcs/3H AQL1.5 C=0Inspection report (PIR A01-002)检验报告(报告编号:A01-002)Close off / Rework隔离 / 返工13highness 高度 2.5+0.2Height Tester0~30mm(01194)高度规3pcs/ Machine start up orChange tool 1pcs/3H AQL1.5 C=0Inspection report (PIR A01-002)检验报告(报告编号:A01-002)Close off / Rework隔离 / 返工12highness 高度 1.2±0.025Height Tester0~30mm(01194)高度规3pcs/ Machine start up orChange tool 1pcs/3H AQL1.5 C=0Inspection report (PIR A01-002)检验报告(报告编号:A01-002)Close off / Rework隔离 / 返工35parallel平行度0.02Dial indicator千分表3pcs/ Machine start up orChange tool 3pcs/3H AQL1.5 C=0Inspection report (PIR A01-002)检验报告(报告编号:A01-002)Close off / Rework隔离 / 返工24Inside diameter 外径Φ13 +0.04Ping gauge 塞规(UGZ-***-0001/UGZ-***-0001)3pcs/ Machine start up orChange tool3pcs/3H AQL1.0 C=0Inspection report (PIR A01-002)检验报告(报告编号:A01-002)Close off / Rework / Scrap隔离 / 返工 / 报废Turning tool 车刀6Outside diameter 外径Rev 转速2500rad/minΦ14.6+0.1Micrometer 千分尺(0~25mm)451384833pcs/ Machine start up orChange tool 1pcs/3H AQL1.5 C=0Inspection report (PIR A01-002)检验报告(报告编号:A01-002)Close off / Rework隔离 / 返工39Roughness 粗糙度F进刀量=0.03mm/r Ra1.6Roughness Tester 粗糙度仪DTS03A3pcs/ Machine start up orChange tool 1pcs/3H AQL1.5 C=0Inspection report (PIR A01-002)检验报告(报告编号:A01-002)Close off / Rework隔离 / 返工28Chamfer 倒角0.2±0.05*45°Projector 投影仪(490127)3pcs/ Machine start up orChange tool 1pcs/3H AQL1.5 C=0Inspection report (PIR A01-002)检验报告(报告编号:A01-002)Close off / Rework隔离 / 返工9highness 高度 3.8+0.1Height Tester0~30mm(01194)高度规3pcs/ Machine start up orChange tool 1pcs/3H AQL1.5 C=0Inspection report (PIR A01-002)检验报告(报告编号:A01-002)Close off / Rework隔离 / 返工29Chamfer 倒角0.2±0.1*45°Projector 投影仪(490127)3pcs/ Machine start up orChange tool 1pcs/3H AQL1.5 C=0Inspection report (PIR A01-002)检验报告(报告编号:A01-002)Close off / Rework隔离 / 返工7highness 高度19.6+0.05/0Height Tester0~30mm(01194)高度规3pcs/ Machine start up orChange tool 1pcs/3H AQL1.5 C=0Inspection report (PIR A01-002)检验报告(报告编号:A01-002)Close off / Rework隔离 / 返工13.Turning Outside Diameter车外圆。
新产品试生产控制程序

1. 目标1. PURPOSE1.1对新产品前期的注塑、喷涂、装配等的过程试验,调试和优化缩短新产品引进过程的周期,确保按时交货,并为新产品进入大批量生产制定优化工艺和程序。
1.1Set up optimize process in Molding, Painting and Assembly to ensure delivery on time andshortest cycle time for new product introduction and ramp up.2. 范围2. SCOPE2.1 适用于本公司所有试生产的通讯塑胶电子类产品2.1 Applicable to all wireless new plastic products.3. 职责3. RESPONSIBILITIES3.1 注塑负责公司制造或外来注塑模具的注塑过程3.1 Molding department is in charge of new product molding process.3.2 喷涂负责新产品喷涂移印过程3.2 Spray painting department is in charge of new product spray painting and pad printing process.3.3 装配负责新产品装配过程3.3 Assembly department is in charge of new product assembling process.3.4 物流部负责提供试生产所需要的原辅材料3.4 Logistic department is in charge of supplying all raw materials for trial run.3.5 物流部计划负责制定、下达试生产计划3.5 Logistic planning department is in charge of new product planning and issuing trial run plan.3.6 工艺工程师负责生产工艺的制定、调整3.6 Process engineer is in charge of setting and improving the process parameter and technology.3.7注塑、喷涂、装配技术员负责按作业计划,根据工艺文件要求进行控制,并和时的掌握信息,反馈给制程工程师、质量部,并负责所使用的现场清洁,负责试生产产品的入库3.7 Molding/spray painting/assembly technician is in charge of operating according to trial run plan,controlling the process according to WI, providing the feedback/information to process engineer and QA in time, keepingthe cleanliness of line and sending trial run productsto storeon time.3.8 质量部负责现场量具和检测设备的控制,检验并确认产品的质量3.8 QA department is in charge of all measuring fixture, gages and testers and ensure product qualitymeet specification.3.9工业工程设备人员负责提供适宜的设备,并对之进行保养、维护、检修。
04_Pre-launch control plan(试生产控制计划)
6
11.38+0.14
NQ-040-67
Altimeter
0.01/0-300
Process checking recorder
1
40%
Measuring instruction paper
Tracing/
Adjustment
/re-checking
Production/ Quality
Incoming material checking records
1
Each batch
Each batch
Separate/
reject
Quality
Material
SAE1215
Chemical composition and Mecs
Incoming material checking records
Prototype样件◄ Pre-launch试生产
Production生产Ctrl. Plan No.控制计划编号2005-10-25-26267
Key Contact/phone联系人/电话
Hou Lai You 86-025-84350565
Date(Orig.)编制日期2005-10-25
Date(rev.)修改日期
1
5%
Measuring instruction paper
Tracing/
Adjustment
/re-checking
Production/ Quality
4
Position
Φ0.14AB
CMM
CMM checking records
1
5%
Measuring instruction paper
生产控制计划常用语中英文双语
生产控制计划(CP)常用语(中英文双语), I; Z; [, o; l8 Z7 \9 E7 }9 N' [4 k* \% @0 y: M. p控制计划(control plan)样本(prototype), }# y. S3 C6 m7 c" S O试生产(pre-launch)生产(production)3 D) k/ T' V( c& W, a控制计划编号(control plan number)6 @9 Q" T5 i( V- K零件号(part number)9 s! g$ G. Z/ H4 `7 l2最新更改水平(latest change level)5 U+ h. f1 N/ }* v57 V零件名称/描述(part name/description). {5 |, j) A5 A5 i- L' i" w1 v供方/工厂(supplier/ plant)供方代码(supplier code)主要联系人/电话(key contact/phone)6 O! X# e8 e& J2 `) Q z, F" P$ K核心小组(core team)/ k' T: u/ a- Q9 |$ `7 X供方/工厂批准/日期(supplier/plant approval/ date)其它批准/日期(如需要)[other approval/ date(if Req’d)], ?% v: y0 B- W, c2 H2 P) X. z日期(编制)[date(orig.)]* X& s) \1 A1 U, W顾客工程批准/日期(如需要)[customer engineering approval/date (if Req’d)]顾客质量批准/日期(如需要)[customer quality approval/date (if Req’d)]& J( I3 T7 D, _( L* I其它批准/日期(如需要)[other approval /date(if Req’d)]日期(修订)[date (Rev.)]零件/过程编号(part /process number)过程名称/操作描述(process name/operation description) 0 `) l+ W# B \( a) z# P! g' l+ m生产设备(machine, device, jig, tools for Mfg.)特性(characteristics) ; g* o# A/ X) M! v M$ Z' F编号(No.) 3 A9 W- ]" S) u9 s产品(product)过程(process)特殊特性分类(special Char. class) : v t* M2 x" |0 A& ]0 D! I产品/过程规范/公差(product/process specification /tolerance)方法(method)评价/测量技术(evaluation / measurement technique)/ }* h( p0 ]: ]7 V3 Y1 @ p样本(sample) ; s4 ~" S' b8 g# ~数量(size) 0 G5 x! w9 V5 C4 h次数(Freq=frequency) 4 z: B' Z- G- c控制方法(control method) - h3 e7 j% X j3 k/ x6 ?& @8 g反应计划(reaction plan): p% q- J8 l( T! n) z* h" j2 P熔料(molten ingot)取样化验分析(sampling inspection)上模(mounting die ) 7 Q3 t. n+ P& k( s/ C, X"调机(machine adjustment)喷脱模剂(spraying release agent)中央溶炉(center furnace) I3 A4 N- A9 x$ V$ X' t+ t/ T冲床(trimming die) 4 M" @4 G) F% E" r, w2 ~目测(visual check) 9 z% K! y7 f5 V' ~7 n7 U6 v' B首检5啤(first inspection for 5 shots)外观(appearance) 4 J& A3 D6 W4 Q5 p9 z, v5黑胚(as-cast)每天一次(once a day) 6 s# F# p9 r5 Y4 t! g3 d连续(continuous)参考控制计划(refer to CP) ! W, b1 S) h. D& E0 m8 j每批(each batch) + v6 P7 d" m: {, _) Q8 v J每次开机(once every operation) : E; w, H3 t7 y) Q6 S厚度(thickness)中心距(c/c =between centers) : w0 d1 r: & c6 b! l+ x孔径(aperture) 9 x- A, r) I' X7 ^& @0 y宽度(width)工序间质量抽查报告(interprocess quality sampling inspection report ) - f. d9 i, j7 @4 \4 K, h) v# j3 A质量首件检查报告(quality first piece inspection report) # ? Z' I* O; q1 U7 b;制程巡回检查报告(processing tour-inspection report)质量追踪分析表(quality traceability analysis report) : g* t8 r& F! V) q. y7 |来料质量抽查报告(incoming quality sampling inspection report) 4 k4 X9 x5 H8 ?* ]6 w; b/ t# @物料标识(material identification) , h8 Q4 b2 ?3 m最终检验质量报告(quality final-inspection report) 2 B. Z. W" u ~3 ~& H, Q' H合金成份化验报告(alloy component assay report) + P0 u3 b& }) e* Q$ I. W2 H- [模具安装检查清单(mounting die inspection sheet)终检(final-inspection)光谱仪(spectrometer)针规(pin gauge ) ! x. T$ p: Y/ T+ {; {电子卡尺(digital calliper) ) |. z5 v9 x3 j W' V5 r* j熔炉温度表(furnace thermometer) 2 C7 g9 `+ k* S( {3 [投影仪(projector)通知生产拉/组长/主管/经理,停机再检查(Inform line/team leader/ supervisor/manager to shut down and recheck )。
控制计划控制程序(中英文)
控制计划控制程序(IATF16949-2016)1、目的1. Purpose对控制零件和过程的体系,通过控制特性的过程监视和控制方法来最大限度地减少过程和产品变差;并随着测量系统和控制方法的评价和改进对其进行修订,使控制计划在整个产品寿命周期中得到保持和使用,确保按顾客的要求制造出优质的产品。
It aims to control the part and process systems and reduce process and product variations to the utmost extent through process monitoring and control methods of the control characteristics; the control plan shall be revised along with the evaluation and improvement of the measurement system and the control methods and shall be maintained and used in the whole product life cycle so as to ensure that high qualify product is manufactured according to the requirements of the customer.2、适用范围2. Scope适用于本公司内产品的样件、小批量试产和批量生产所用的控制计划。
如客户有特殊要求,必须按照客户的要求执行。
It applies to the control plans used in the product sample, small-lot trial production and volume production of the company. If the customerhas special requirements, it shall be implemented according to the requirements of the customer.3、定义3. Definition无None4、职责4. ResponsibilitiesAPQP项目小组负责控制计划的策划,质量部负责编制与维护The APQP project team shall be responsible for planning of the control plan and the quality department shall be responsible for preparation and maintenance of it.5、程序5. Procedure5.1 当顾客和公司有需求和要求时,项目小组在不同阶段制订出相应的控制计划(即:样件控制计划、试生产控制计划、生产控制计划),项目组按工艺文件将其发行至相关部门,由其执行。
生产控制程序 英语流程
生产控制程序英语流程Production Control Program English FlowchartProduction planning is a crucial aspect of any manufacturing or industrial operation. It involves the coordination of various processes and resources to ensure efficient and cost-effective production. One of the key components of production planning is the implementation of a production control program, which helps to monitor and regulate the flow of materials, the utilization of equipment, and the overall productivity of the manufacturing process.The production control program typically consists of several interconnected components, each serving a specific purpose. These components include forecasting, capacity planning, scheduling, inventory management, and quality control. By integrating these elements, the production control program aims to optimize the production process and maximize the output while minimizing waste and inefficiencies.Forecasting is the first step in the production control program. This involves analyzing historical data, market trends, and customer demand to predict future production requirements. Accurateforecasting enables the organization to plan ahead and allocate resources accordingly, ensuring that the right products are manufactured at the right time to meet customer needs.Capacity planning is the next step in the process. This involves determining the production capacity of the manufacturing facility, taking into account factors such as equipment capabilities, labor availability, and production constraints. By understanding the production capacity, the organization can make informed decisions about production scheduling, resource allocation, and potential expansion or investment in new equipment.Scheduling is a critical component of the production control program. It involves the development of a detailed production plan that outlines the sequence and timing of various production activities. This includes the allocation of resources, the coordination of production processes, and the management of material flow. Effective scheduling helps to minimize downtime, reduce bottlenecks, and ensure the timely delivery of products to customers.Inventory management is another crucial aspect of the production control program. This involves the monitoring and control of raw materials, work-in-progress, and finished goods inventory. Efficient inventory management helps to maintain the right balance between supply and demand, minimizing the risk of stockouts or excessiveinventory levels. This, in turn, can lead to cost savings and improved cash flow for the organization.Quality control is the final component of the production control program. This involves the implementation of various quality assurance measures to ensure that the final products meet the required standards and specifications. Quality control activities may include inspection, testing, and continuous improvement initiatives. By maintaining a high level of quality, the organization can enhance customer satisfaction, reduce the risk of product recalls, and maintain a competitive advantage in the market.The production control program is typically implemented through the use of various software tools and technologies, such as Enterprise Resource Planning (ERP) systems, Manufacturing Execution Systems (MES), and Production Planning and Control (PPC) software. These systems integrate the various components of the production control program, providing real-time data and analytics to support decision-making and optimize the production process.In conclusion, the production control program is a comprehensive and integrated approach to managing the production process. By incorporating forecasting, capacity planning, scheduling, inventory management, and quality control, organizations can achieve greater efficiency, cost-effectiveness, and customer satisfaction. The effectiveimplementation of a production control program is a critical factor in the success of any manufacturing or industrial operation.。