
抽样作业指导书 Sampling Plan for Inspection Instruction
抽样作业指导书 Sampling Plan for Inspection Instruction
Rev. AA
Ori. Date Doc No. Page Page1of 9
Type WI *** Company Limited Dept. Record of Revision: No. Rev Originator Summaries Date CCF No. 1 2 3 4 5 6 7 8 9 10
DISTRIBUTION: Department Organization 抽样作业指导书 Sampling Plan for Inspection Instruction
Rev. AA
Ori. Date Doc No. Page Page2of 9
Type WI *** Company Limited Dept. 1. Purpose 目的 This instruction serves to standardize the sampling standard applying ANSI/ASQC Z1.4 to conduct incoming materials and finish goods inspections, ensuring products meeting quality requirements.
本规程旨在规范使用ANSI/ASQC Z1.4单次抽样法对来料进行抽样检验,确保品质符合规范要求。
2. Scope 适用范围 This document is applicable to the inspection of all production materials and finished goods of *** Company Limited Plant. 本规程适用于***有限公司所有生产物料和成品的检查。
3. Responsibility职责 Quality Manager has the responsibility and authority to implement this procedure wherever sampling is required
品质经理赋予全权负责执行此流程。
4. Definition定义 AQL: Acceptable Quality Level 可接收质量水平。 Ac: Accept 接受 Re: Reject 拒收 CR: Critical 致命缺陷,会对人员造成伤害或火灾等。 MA: Major 严重缺陷,对产品有重大影响的缺陷。 MI: Minor 轻微缺陷,对产品有影响的缺陷。
5. Procedures作业程序 5.1 Inspection Levels 检查水平的规定: There are three general inspection levels (I, II & III) and four special inspection levels (S-1, S-2, S-3 & S-4).
检查水平分:一般检查水平(I、II、III)和特殊检查水平(S-1、S-2、S-3、S-4)。 Unless otherwise specified, Inspection Level II will be used. However, Inspection Level I 抽样作业指导书 Sampling Plan for Inspection Instruction
Rev. AA
Ori. Date Doc No. Page Page3of 9
Type WI *** Company Limited Dept. may be specified when less discrimination is needed, or Level III may be specified for greater discrimination. Four additional special levels: S-1, S-2, S-3, and S-4, are given in the same table and may be used where relatively small sample sizes are necessary and large sampling risks can or must be tolerated..
除非另有规定,通常采用一般检查水平 II 。当需要的判别力比较低时,可规定使用一般检查水平 I ,当需要的判别力比较高时,可规定使用一般检查水平 III 。特殊检查水平仅适用于必须使用较小的样本,而且能够或必须允许较大的误判风险。
Individual Inspection levels are designated per category of non-conforming in principle, it should be noted that inspection levels correspond with acceptance level of quality.
原则上按不合格的分类分别规定检查水平,但必须注意检查水平与合格质量水平之间的协调一致。 NOTE: In the designation of inspection levels S-1 to S-4, care must be exercised to avoid AQLs inconsistent with these inspection levels. For example, To correspond with the maximum sample size of single sampling plan for normal inspection exceeds 8 if sample size did not exceed D in S-1 level. If specified AQL =0.10, then the smaller sample sizes of single sampling plan for normal inspection is 125, therefore, S-1 shall be not to be used under AQL=0.10.
注:在规定特殊检查水平S-1至S-4时,必须注意避免检查水平同所规定的合格质量水平之间的矛盾。例如,在S-1中,样本大小字码没有超过 D,相当于正常一次抽样方案样本大小最多等于8。若规定AQL=0.10,则正常检查一次抽样方案的最小样本大小为125。因此,在规定AQL=0.10的情况下,不能规定使用特殊检查水平S-1。
5.2 Normal, Tightened and Reduced Inspection 检查严格度的确定: Generally, there are three grades for inspection –normal , tightened and reduced. Normal inspection will be used at the start of inspection unless otherwise directed by the responsible authority.
检查的严格度是指提交批所接受检查的宽严程度,通常规定为---正常检查、加严检查和放宽检查三种不同严格度的检查。除非另有规定,在检查开始时应使用正常检查。
5.3 Switching Procedures 转移规则: 5.3.1 Normal to Tightened 从正常检查到加严检查 When normal inspection is in effect, tightened inspection shall be instituted when 3 out of 5 or fewer consecutive lots or batches have been non-acceptable on original inspection. 当进行正常检查时,若在连续检查五批中有三批以上(不包括再次提交检查批)不合格,则从下一批检查转到加严检查。
5.3.2 Tightened to Normal 从加严检查到正常检查 When tightened inspection is in effect, normal inspection shall be instituted when 5 consecutive lots or batches have been considered acceptable on original inspection. 抽样作业指导书 Sampling Plan for Inspection Instruction
Rev. AA
Ori. Date Doc No. Page Page4of 9
Type WI *** Company Limited Dept. 当进行加严检查时,若连续检验五批结果均(不包括再次提交检查批)合格,则从下一批检查转到正常检查。
5.3.3 Normal to Reduced 从正常检查到放宽检查 When normal inspection is in effect, reduced inspection shall be instituted providing that all of the following conditions are satisfied. a. The preceding 10 lots or batches (or more) have been on normal inspection and all have been accepted on original inspection; and b. The total number of nonconforming units (or nonconformities) in the samples from the preceding 10 lots or batches (or such other number as was used for condition “a” above) is equal to or less than the applicable limit number; and c. For Hi-tech products with at a steady rate; such as IC, resistor and capacitor; and d. Production is at a steady rate, reduced inspection is considered desirable by quality manager. 当进行正常检查时,若下列条件均满足,则从下一批转到放宽检查。
IQC来料检验作业指导书(中英文)

IQC来料检验作业指导书Incoming_Inspection_Work_Instruction文件更改历史记录Amendment History版次Revision更改日期Change Date更改概要Description of Changes更改人Prepared by批准人Approved byPrepared by编制Reviewed by审核Approved by批准来料检验作业指导书Incoming_Inspection_Work_Instruction1.0Purpose目的The objective of this procedure is to define a standard inspection method in performing inspection and testing of components or materials.本程序目的在于定义对元件或材料进行检验/测试的标准操作方法。
Scope适用范围This procedure is applicable to all components and materials that require the relevant inspection and testing, as specified in the individual Part or Material Specification.本程序适用于所有按照元件和材料规格进行检验和测试的元件和材料。
2.0Sampling / Equipment Used 取样 / 使用设备2.1Per sampling plan stated in the Incoming Inspection Procedure: AQL:MA=0.4、MI=1.0按照来料检验程序所规定的抽样计划;AQL:MA=0.4、MI=1.0级别进行抽样.2.2Inspection Aids检验工具4.2.1 LCR Meter / LCR 测量仪4.2.2 Fluke Multimeter / Fluke 万用表4.2.3 Caliper / Plug Gauge / Pin Gauge / 游标卡尺/ 塞规/针规4.2.4 Magnifier / Microscope / 放大镜 / 显微镜3.0Reference Documents参考文件3.1 Customer’s AVL / 客户接受的供应商清单3.2 Manufacturer Part Specification / 供应商的元件规格。
【最新文档】作业指导书英文-范文word版 (8页)

本文部分内容来自网络整理,本司不为其真实性负责,如有异议或侵权请及时联系,本司将立即删除!== 本文为word格式,下载后可方便编辑和修改! ==作业指导书英文篇一:PFMEA作业指导书(中英文)德信诚培训网PFMEA作业指导书1 PURPOSE(目的)The purpose of this work instruction is to provide a method for continuous improvement through the use of PFMEAs.此作业指导书的目的是为运用制程失效模式及效果分析达到持续改善目的提供方法。
2 SCOUPE(范围)This work instruction applies to any manufacturing process that has a customer requirement for failure mode effect analysis or any process at FLEX (Doumen) where management requires a PFMEA.适用于客户要求或管理要求而需要做失效模式及效果分析的所有制程。
3 DEFINITIONS(定义)3.1 PFMEA: Process Failure Mode and Effect Analysis. It should describe all thepotential failure modes which may occur in process and their corresponding failure effects; evaluate and rank the severity, occurrence and detection of the failures. It should also describe the current control method, recommend corrective action, person responsible responsibility and due date.PFMEA--制程失效模式及效果分析。
AQL 抽样指导书
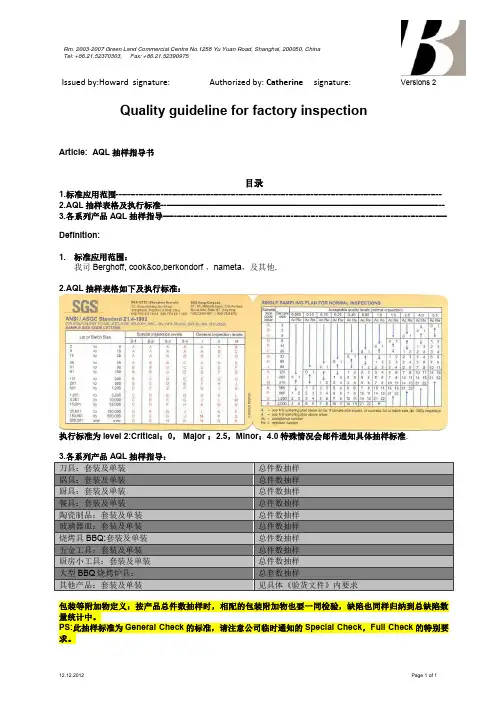
Rm. 2003-2007 Green Land Commercial Centre No.1258 Yu Yuan Road, Shanghai, 200050, ChinaTel: +86.21.52370303, Fax: +86.21.52390975Issued by:Howardsignature: Authorized by: Catherine signature: Versions 212.12.2012 Page 1 of 1Quality guideline for factory inspectionArticle: AQL 抽样指导书目录1.标准应用范围┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄2.AQL 抽样表格及执行标准┄┈┈┈┈┈┈┈┈┈┈┈┈┈┈┈┈┈┈┈┈┈┈┈┈┈┈┈┈┈┈┈┈┄3.各系列产品AQL 抽样指导┈┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┈Definition:1. 标准应用范围:我司Berghoff, cook&co,berkondorf ,nameta ,及其他.2.AQL 抽样表格如下及执行标准:执行标准为level 2:Critical :0, Major :2.5,Minor :4.0特殊情况会邮件通知具体抽样标准. 3.各系列产品AQL 抽样指导:刀具:套装及单装 总件数抽样锅具:套装及单装 总件数抽样厨具:套装及单装 总件数抽样餐具:套装及单装 总件数抽样陶瓷制品:套装及单装 总件数抽样玻璃器皿:套装及单装 总件数抽样烧烤具BBQ:套装及单装 总件数抽样五金工具:套装及单装 总件数抽样厨房小工具:套装及单装 总件数抽样大型BBQ 烧烤炉具: 总套数抽样其他产品:套装及单装 见具体《验货文件》内要求包装等附加物定义:按产品总件数抽样时,相配的包装附加物也要一同检验,缺陷也同样归纳到总缺陷数量统计中。
【推荐】检验指导书英文简称-范文模板 (6页)
本文部分内容来自网络整理,本司不为其真实性负责,如有异议或侵权请及时联系,本司将立即删除!== 本文为word格式,下载后可方便编辑和修改! ==检验指导书英文简称篇一:ISO9001进料检验作业指导书(中英文)ISO9001进料检验作业指导书 Incoming_Inspection_Work_Instruction文件更改历史记录Amendment HistoryISO9001进料检验作业指导书 Incoming_Inspection_Work_Instruction1.0 Purpose目的The objective of this procedure is to define a standard inspection method in performing inspection and testing of components or materials. 本程序目的在于定义对元件或材料进行检验/测试的标准操作方法。
Scope适用范围This procedure is applicable to all components and materials that require the relevant inspection and testing, as specified in the individual Part or Material Specification.本程序适用于所有按照元件和材料规格进行检验和测试的元件和材料。
2.0 Sampling / Equipment Used 取样 / 使用设备2.1 Per sampling plan stated in the Incoming Inspection Procedure:(来自: : 检验指导书英文简称 ) AQL:MA=0.4、MI=1.0按照来料检验程序所规定的抽样计划;AQL:MA=0.4、MI=1.0级别进行抽样. 2.2 Inspection Aids检验工具4.2.1 LCR Meter / LCR 测量仪4.2.2 Fluke Multimeter / Fluke 万用表4.2.3 Caliper / Plug Gauge /Pin Gauge / 游标卡尺/ 塞规/针规 4.2.4 Magnifier / Microscope / 放大镜/ 显微镜3.0 Reference Documents参考文件3.1 Customer’s AVL / 客户接受的供应商清单3.2 Manufacturer Part Specification / 供应商的元件规格篇二:IQC来料检验作业指导书(中英文)IQC来料检验作业指导书Incoming_Inspection_Work_Instruction文件更改历史记录Amendment History来料检验作业指导书Incoming_Inspection_Work_Instruction1.0 Purpose目的The objective of this procedure is to define a standard inspection method in performing inspection and testing of components or materials. 本程序目的在于定义对元件或材料进行检验/测试的标准操作方法。
SOP-QA-001-D-来料检验作业指导书-Incoming-Inspection-Work-Instruction

Co-approved by: 审核人:赵桂林
Approved by: 批准人:
Title: engineer 职位:工程师
Title: 职位:质量主管
Title: 职位:
Signature: 签名:
Signature: 签名:
Signature: 签名:
5.0 Inspection Criteria / 检验要点
5.1 MFG AVL Verification / 生产厂商确认 Verify that the parts are from the authorized vendor per AVL list. 根据 AVL 清单验证元件是否为承认厂商。
7 剥皮测试检查供应商出货报告内容是否有阻焊膜粘贴性试验 是否 OK
8 Visual check 外观检查
a. Surface checking with naked eyes 裸眼作表面可视性检查
b. Use 5X/8X magnifier check the defect area 用五至八倍放大镜对有缺陷可能的位置进行检查
5.2 MFG Part Number Verification / 生产厂商料号确认 Verify that manufacturer part number and description are correct per PO and DO. 根据 PO 和 DO 验证生产厂家料号和元件种类 .
根各元件的规格对抽样样品进行尺寸检验; 记录 5 个检验数据;
5.6 Part Value Measurement / 测值 For inductors/capacitors/resistors, need to perform value measurements using LCR meter that record 5PCS per datecode according to AVL and manufacturer ’spsecifications. 5 data to be recorded. 对于电感 /电容 /电阻元件,需按照 AVL 和厂家的标准,利用 L/C/R 测量仪进行测值, 每
TS16949来料检验作业指导书(中英文)

TS16949来料检验作业指导书Incoming_Inspection_Work_Instruction文件更改历史记录Amendment History版次Revision更改日期Change Date更改概要Description of Changes更改人Prepared by批准人Approved byPrepared by编制Reviewed by审核Approved by批准TS16949来料检验作业指导书Incoming_Inspection_Work_Instruction1.0Purpose目的The objective of this procedure is to define a standard inspection method in performing inspection and testing of components or materials.本程序目的在于定义对元件或材料进行检验/测试的标准操作方法。
Scope适用范围This procedure is applicable to all components and materials that require the relevant inspection and testing, as specified in the individual Part or Material Specification.本程序适用于所有按照元件和材料规格进行检验和测试的元件和材料。
2.0Sampling / Equipment Used 取样 / 使用设备2.1Per sampling plan stated in the Incoming Inspection Procedure: AQL:MA=0.4、MI=1.0按照来料检验程序所规定的抽样计划;AQL:MA=0.4、MI=1.0级别进行抽样.2.2Inspection Aids检验工具4.2.1 LCR Meter / LCR 测量仪4.2.2 Fluke Multimeter / Fluke 万用表4.2.3 Caliper / Plug Gauge / Pin Gauge / 游标卡尺/ 塞规/针规4.2.4 Magnifier / Microscope / 放大镜 / 显微镜3.0Reference Documents参考文件3.1 Customer’s AVL / 客户接受的供应商清单3.2 Manufacturer Part Specification / 供应商的元件规格3.3 Yamaoka AVL List / 本公司的AVL3.4 QAP-010 : Incoming Inspection Procedure / 来料检验程序3.5 SOP-QA-003 : Material Aging Control Procedure / 物料保质期控制程序4.0Inspection Criteria / 检验要点4.1MFG AVL Verification / 生产厂商确认Verify that the parts are from the authorized vendor per AVL list.根据AVL清单验证元件是否为承认厂商。
Control Plan Management Procedure(中英文)
Control Plan Management ProcedureTS16949控制计划管理程序1.0 目的Purpose:指导产品的生产过程在一个受控制环境下进行,及发生不良时应采取相应处理方案。
Ensure production to be carried out under a controlled environment,and to establish action plans to deal with occurrence of defects.2.0 范围Scope:本程序适用于产品生产过程控制。
This procedure is applicable to product’s production process control。
3.0 定义Definition:3.1 CP ---控制计划 Control Plan3.2 DCC --- 文件控制中心 Document Control Center4.0 职责Responsibilities:4.1工程部负责核查客户提供的资料和信息Engineering department is responsible to verify information and data supplied by customers4.2所有相关部门等审核,批准控制计划All the concerned departments shall audit and approve the control plan4.3 IPQC监控控制计划执行情况IPQC shall monitor the execution status of the control plan5.0 程序Procedure:5.1 工程部负责核查客户提供的资料,并要求客户提供需要的辅助资料 .Engineering department is responsible audit customer supplied information, and request customer to supply necessary supplementary information .5.2 收集所有的资料后,工程部在这些资料的基础上制定最初的控制计划, 并和个人化、质检部、封装部PMC等部门开会协商,讨论满足客户需求的质量行动及涉及的财务问题。
AQL抽样计划使用操作指引
b、主要缺陷AQL=0.4时,箭头朝上n=32;Ac=0, Re=1;次要缺陷AQL=1.5时,n=50;Ac=2,Re=3。
c、依据确定样本量大小原则:所选样本量与主要缺陷及次要缺陷相交时必须都有判定数组[Ac, Re]的数值,由此可得出:正常检查一次抽样方案为:n=32;
生效日期
Effective Date
V0
新 版 发 行
编 写 人:
Prepared by
审 批 人:
Approved by
如此印章并非红色, IF THE CONTROL STAMP
表此文件并非合法之版 COLOR IS NOT RED ,THEN IT
本,并不会受到控制及 IS AN UNCONTROLLED COPY.
6.11检查样本
根据产品规格或合同中对单位产品规定的检验项目,逐个对样本单位进行检查,并累计不合格品总数或不合格总数(当有缺陷分类时应分开累计).
6.12 检查合格或不合格的判断
6.12.1 根据质量允收水准(AQL)和检查水平(IL)确定的抽样方案,用6.7.2、6.7.3提供的方法进行判断,只有按所确定的抽样方案全部判断是合格的,才能最终判断该检查批逐批检查合格;否则就判该检查批逐批不合格。
4.8 检验项目----产品品质特性里所特定需要检验的项目。
4.9 不良品---- 如果产品有一个或一个以上的检验项目不合格时, 那么这个产品为不良品。
4.10 良品----全部检验项目都合符规格的产品。
4.11 过程平均----一系列初次提交检查批的平均质量(用每百单位产品不合格品数或每百单位产品不合格数表示)其中初次提交检查批不包括第一次提交检查判为不合格,重工后再次提交检查的批。
出入境食品抽采样作业指导书
出入境食品抽/采样作业指导书版本号:B版发布日期:2007.11.12文件编号:BJQS31006180(非受控)编写人:食品处审核人:法综处批准人:伦立广中华人民共和国北京出入境检验检疫局BEIJING ENTRY-EXIT INSPECTION AND QUARANTINE出入境食品抽/采样作业指导书1.目的为统一规范北京地区出入境食品检验检疫抽/采样工作,确保出入境食品检验监督工作质量,特制定本作业指导书。
2.适用范围本作业指导书适用于北京地区出入境食品检验检疫抽/采样工作的质量控制。
3.职责3.1食品监管处负责管理北京地区出入境食品检验检疫抽/采样工作。
3.2各口岸分支机构负责本口岸出入境食品检验检疫抽/采样工作。
3.3动植食处负责经国际邮局邮寄入境的食品检验检疫抽/采样工作。
4.依据4.1《中华人民共和国食品卫生法》4.2《中华人民共和国进出口商品检验法》4.3《中华人民共和国进出口商品检验法实施条例》(2005年8月31日国务院447号令)4.4《检验检疫工作手册》(〈植物源性食品、深加工食品分册〉、〈动物源性食品、食品包装及化妆品分册〉,国家质检总局2006年版)4.5《进口食品卫生监督检验工作规程》5.作业要点施检人员经过现场查验后,应根据食品的不同种类、品种、包装形式和检验要求实施抽/采样。
抽/采样要有充分的代表性。
从样品的采集至送抵实验室的整个过程不得有任何污染,确保样品的真实性。
5.1抽/采样操作的原则5.1.1应按照随机规则抽/采样。
不能有意识地只抽好的或差的,特殊需要的例外。
5.1.2抽/采样的部位应具有代表性。
应从批的整体中各部位抽取,如从四角+中间;分上、中、下层;或上、中上、中、中下、下层;梅花点式等。
5.1.3抽样的数量能充分代表批的整体。
除了按照理论的抽样数量抽取外,也可根据实践经验和既往质量史等具体情况掌握。
5.1.4抽/采样工具和容器必须清洁、干燥、无异味,不得将有害物质带入样品中。
【精编范文】检验作业指导书英文-word范文 (6页)
本文部分内容来自网络整理,本司不为其真实性负责,如有异议或侵权请及时联系,本司将立即删除!== 本文为word格式,下载后可方便编辑和修改! ==检验作业指导书英文篇一:ISO9001进料检验作业指导书(中英文)ISO9001进料检验作业指导书 Incoming_Inspection_Work_Instruction文件更改历史记录Amendment HistoryISO9001进料检验作业指导书 Incoming_Inspection_Work_Instruction1.0 Purpose目的The objective of this procedure is to define a standard inspection method in performing inspection and testing of components or materials. 本程序目的在于定义对元件或材料进行检验/测试的标准操作方法。
Scope适用范围This procedure is applicable to all components and materials that require the relevant inspection and testing, as specified in the individual Part or Material Specification.本程序适用于所有按照元件和材料规格进行检验和测试的元件和材料。
2.0 Sampling / Equipment Used 取样 / 使用设备2.1 Per sampling plan stated in the Incoming Inspection Procedure: AQL:MA=0.4、MI=1.0按照来料检验程序所规定的抽样计划;AQL:MA=0.4、MI=1.0级别进行抽样. 2.2 Inspection Aids检验工具4.2.1 LCR Meter / LCR 测量仪4.2.2 Fluke Multimeter / Fluke 万用表4.2.3 Caliper / Plug Gauge /Pin Gauge / 游标卡尺/ 塞规/针规 4.2.4 Magnifier / Microscope / 放大镜/ 显微镜3.0 Reference Documents参考文件3.1 Customer’s AVL / 客户接受的供应商清单3.2 Manufacturer Part Specification / 供应商的元件规格篇二:ISO9001-201X进料检验作业指导书(中英文)进料检验作业指导书Incoming_Inspection_Work_Instruction(ISO9001:201X)1.0 Purpose目的The objective of this procedure is to define a standard inspection method in performing inspection and testing of components or materials. 本程序目的在于定义对元件或材料进行检验/测试的标准操作方法。